Skip to content
Made in France since 1948 · Vire, Normandy +33 (0)2 31 66 44 00
Guy Degrenne Industrie Request a quote
Stainless steel industrial subcontracting · Vire, Normandy

Technologies and machinery.

Stainless steel subcontractor since 1967: twelve areas of expertise, from deep drawing to gold and silver electroplating, plus Limoges and Alföld porcelain. Here is everything our master deep drawers, toolmakers, polishers and silversmiths can do, and with which machines.

Stainless steel304 (18/10) · 430 (18/0)
Precious metalsGold · Silver
PorcelainLimoges · Alföld
SeriesPrototype → millions
01 · Design

The part validated before the first press stroke.

Our engineering office works with your technical teams, from complex aesthetic parts to demanding mechanical components.

Animated diagram
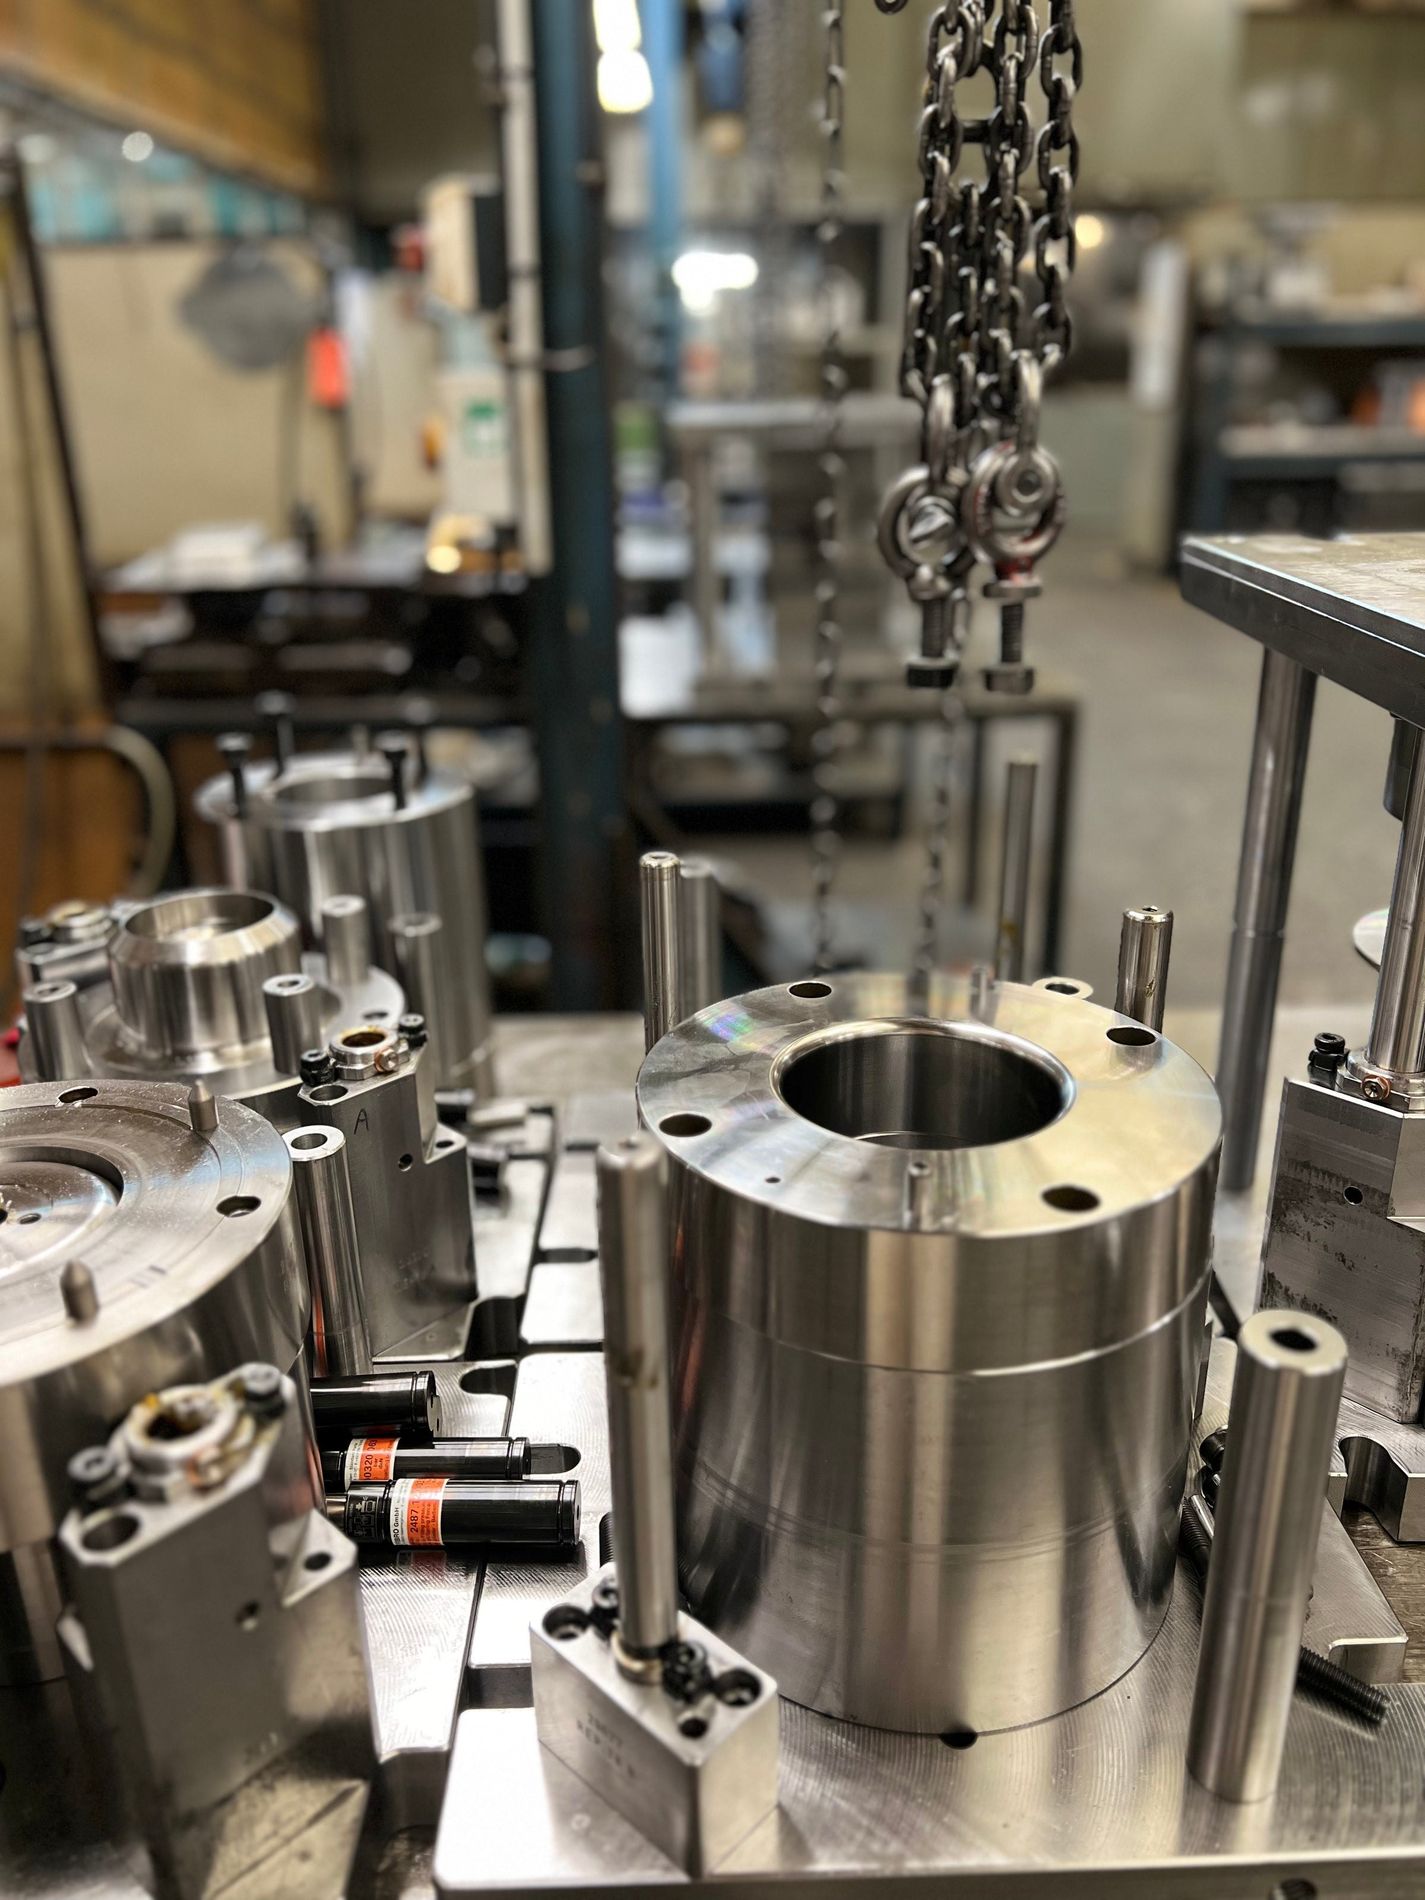
Press tooling in the Vire workshop
In the Vire workshopPress tooling in the Vire workshop
Engineering office

Design and numerical simulation

Every project goes through the engineering office before industrialisation. Simulation identifies risk areas (thinning, wrinkles, tears) and the process or tool is corrected before the first trial.

  • IBlank and tools meshed from the CATIA CAD model
  • IIDrawing simulation, increment by increment
  • IIIThickness map: thinned and thickened areas
  • IVValidated simulation: tooling designed and made in Vire
CAD
CATIA
Simulation
Multi-pass, with or without springback calculation
Result
Shorter and cheaper tryout
Prototyping

Steel prototypes, 3D printed

Hold the part in your hand before launching the tool. Our metal prototypes are printed by laser powder bed fusion in steel powder.

  • IThe recoater spreads a layer of steel powder
  • IILaser fusion layer after layer, on supports
  • IIIDepowdering, then removal from the build plate
  • IVShape and handling validated with you
Process
Laser powder bed fusion (SLM)
Material
Steel powder
Use
Prototypes before tooling
Animated diagram
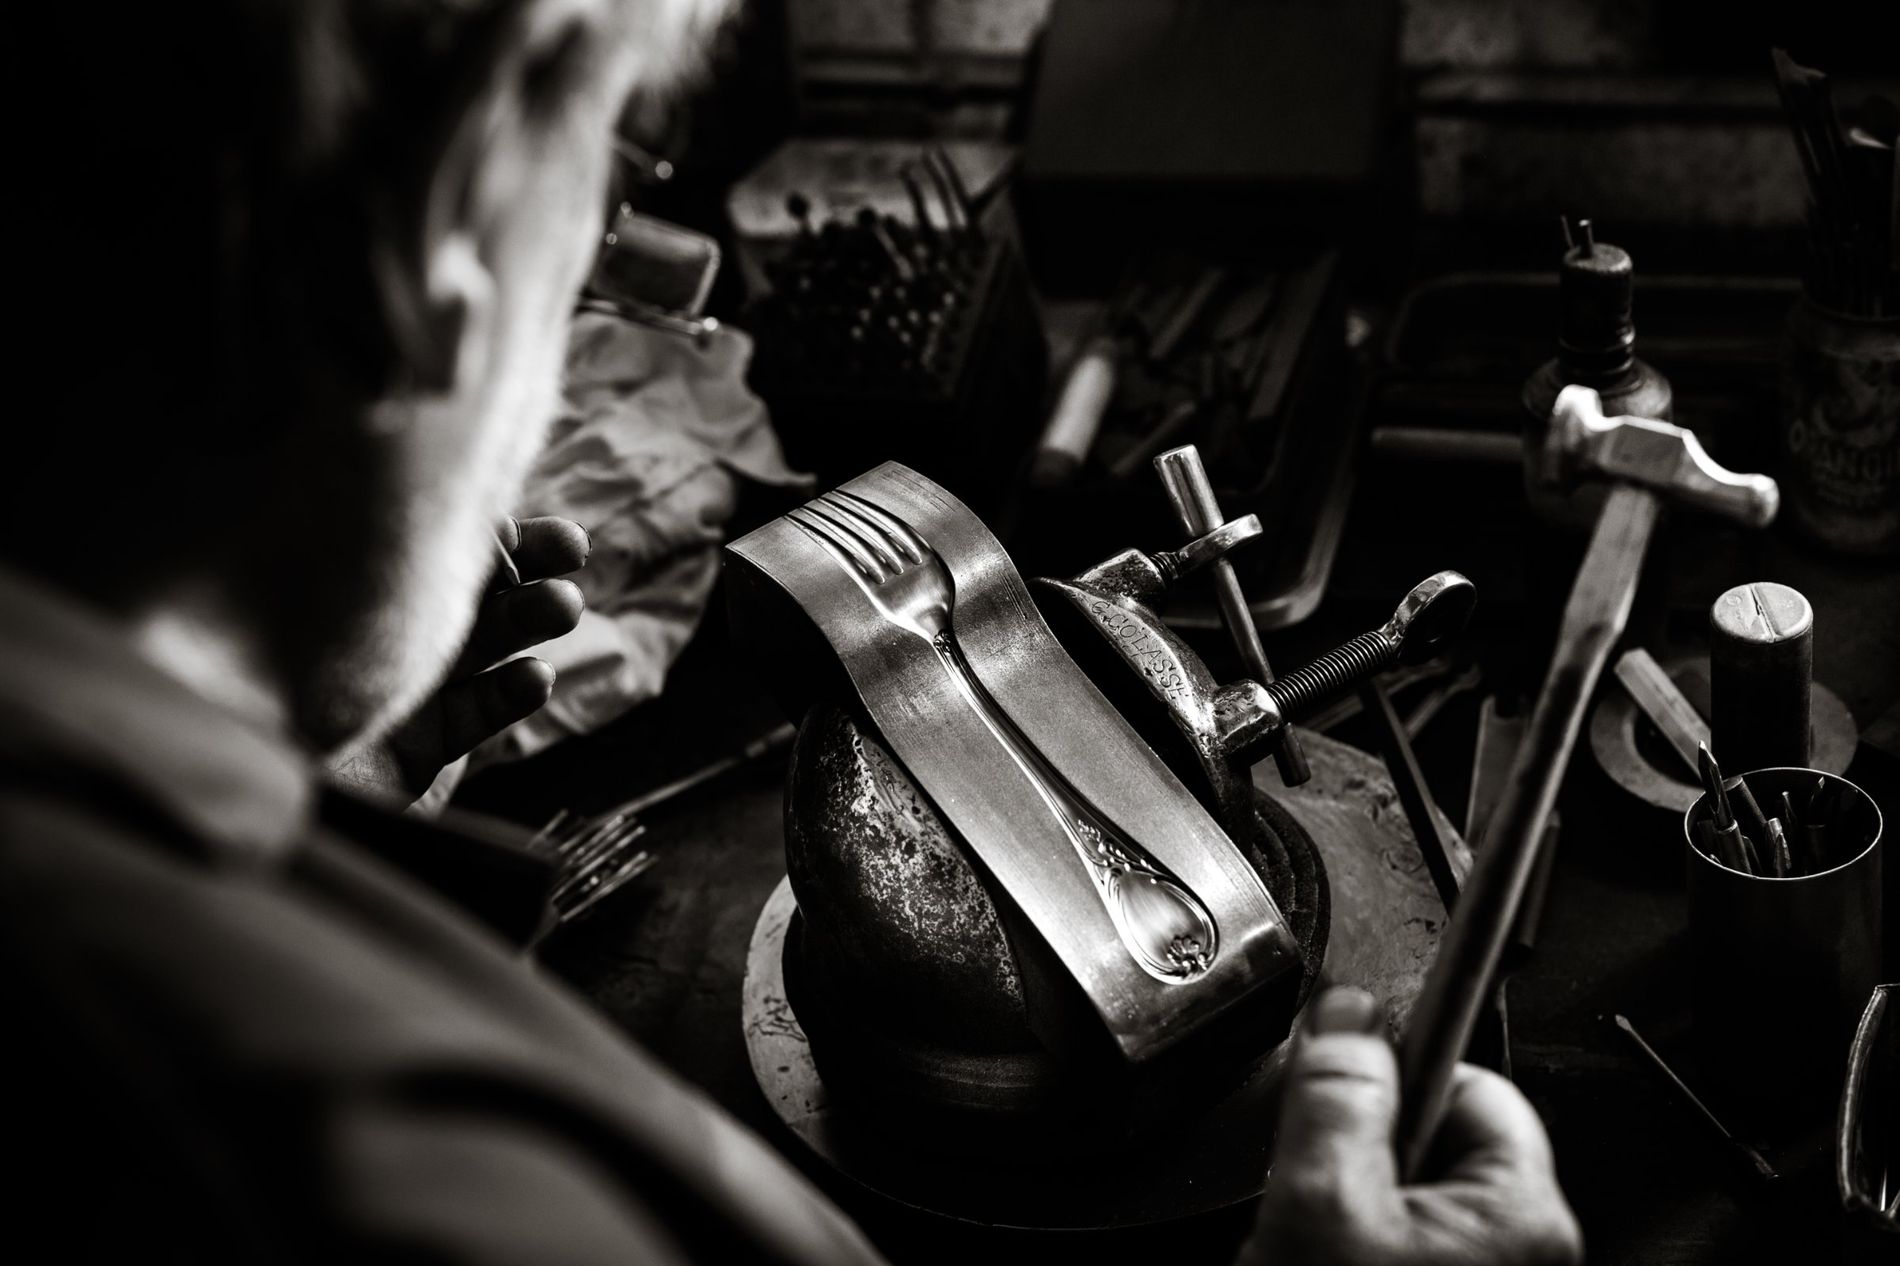
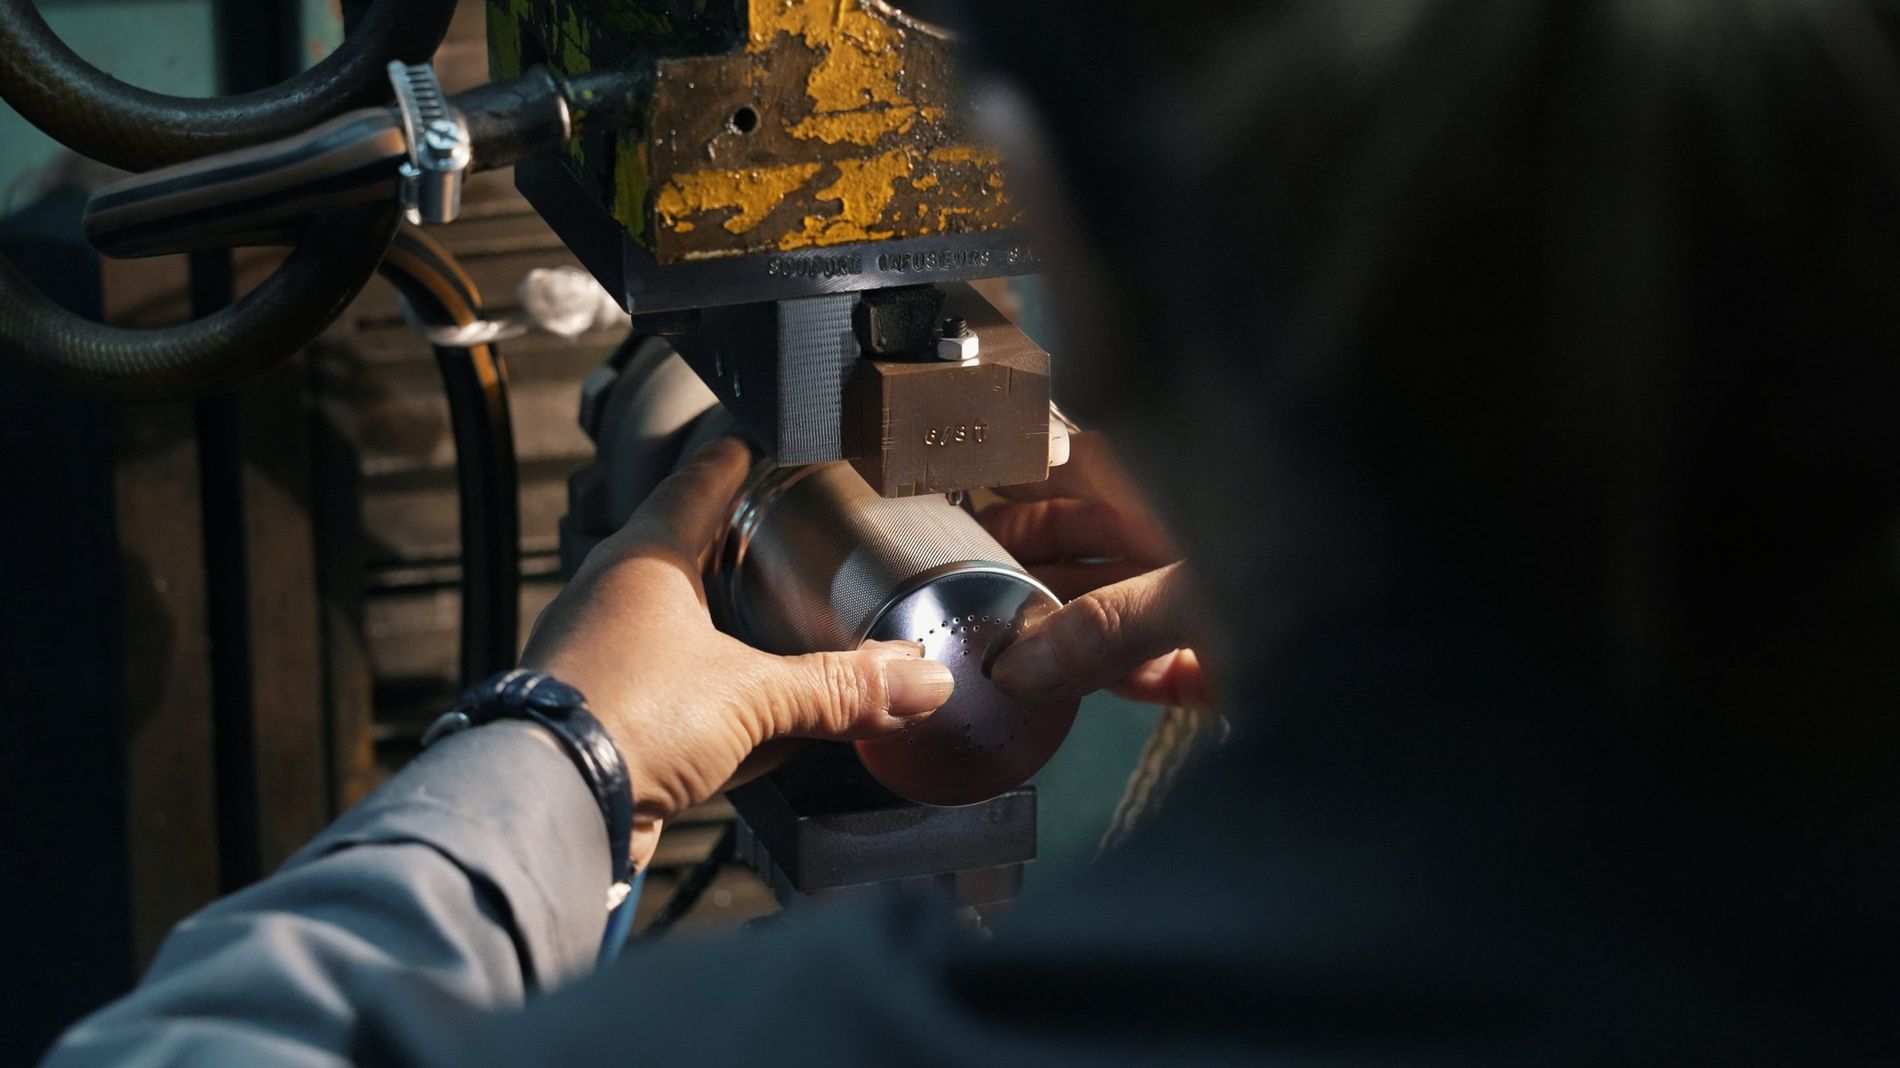
Engraver working on a stamping die
Tooling

Dies and tools made in Vire

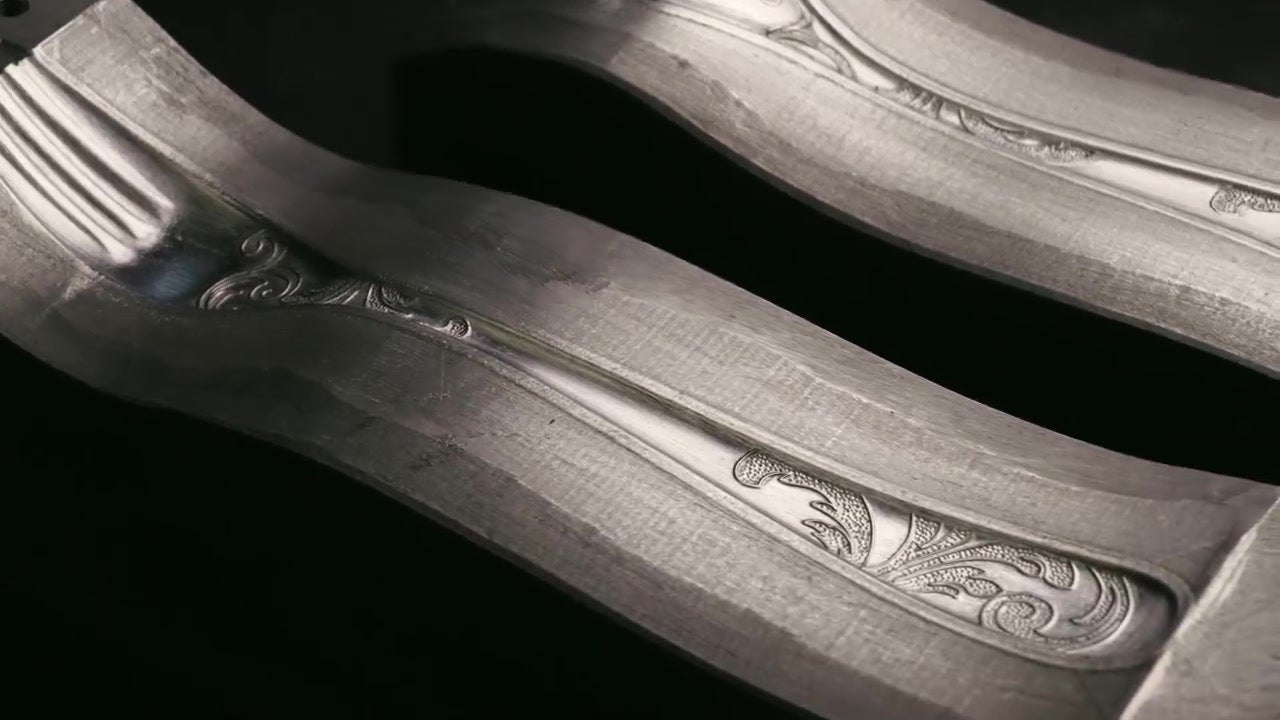
Our tools are designed and made in-house, with our own machining resources. Flatware stamping dies are engraved by hand.

  • IDrawing, sizing and cutting tools
  • IIProgressive dies
  • IIIEngraved stamping dies
  • IVOn-site tool maintenance and rework
Resources
Machining dedicated to tooling
Ownership
Client-owned tooling possible, under NDA
02 · Forming

From flat sheet to hollow part, in one piece.

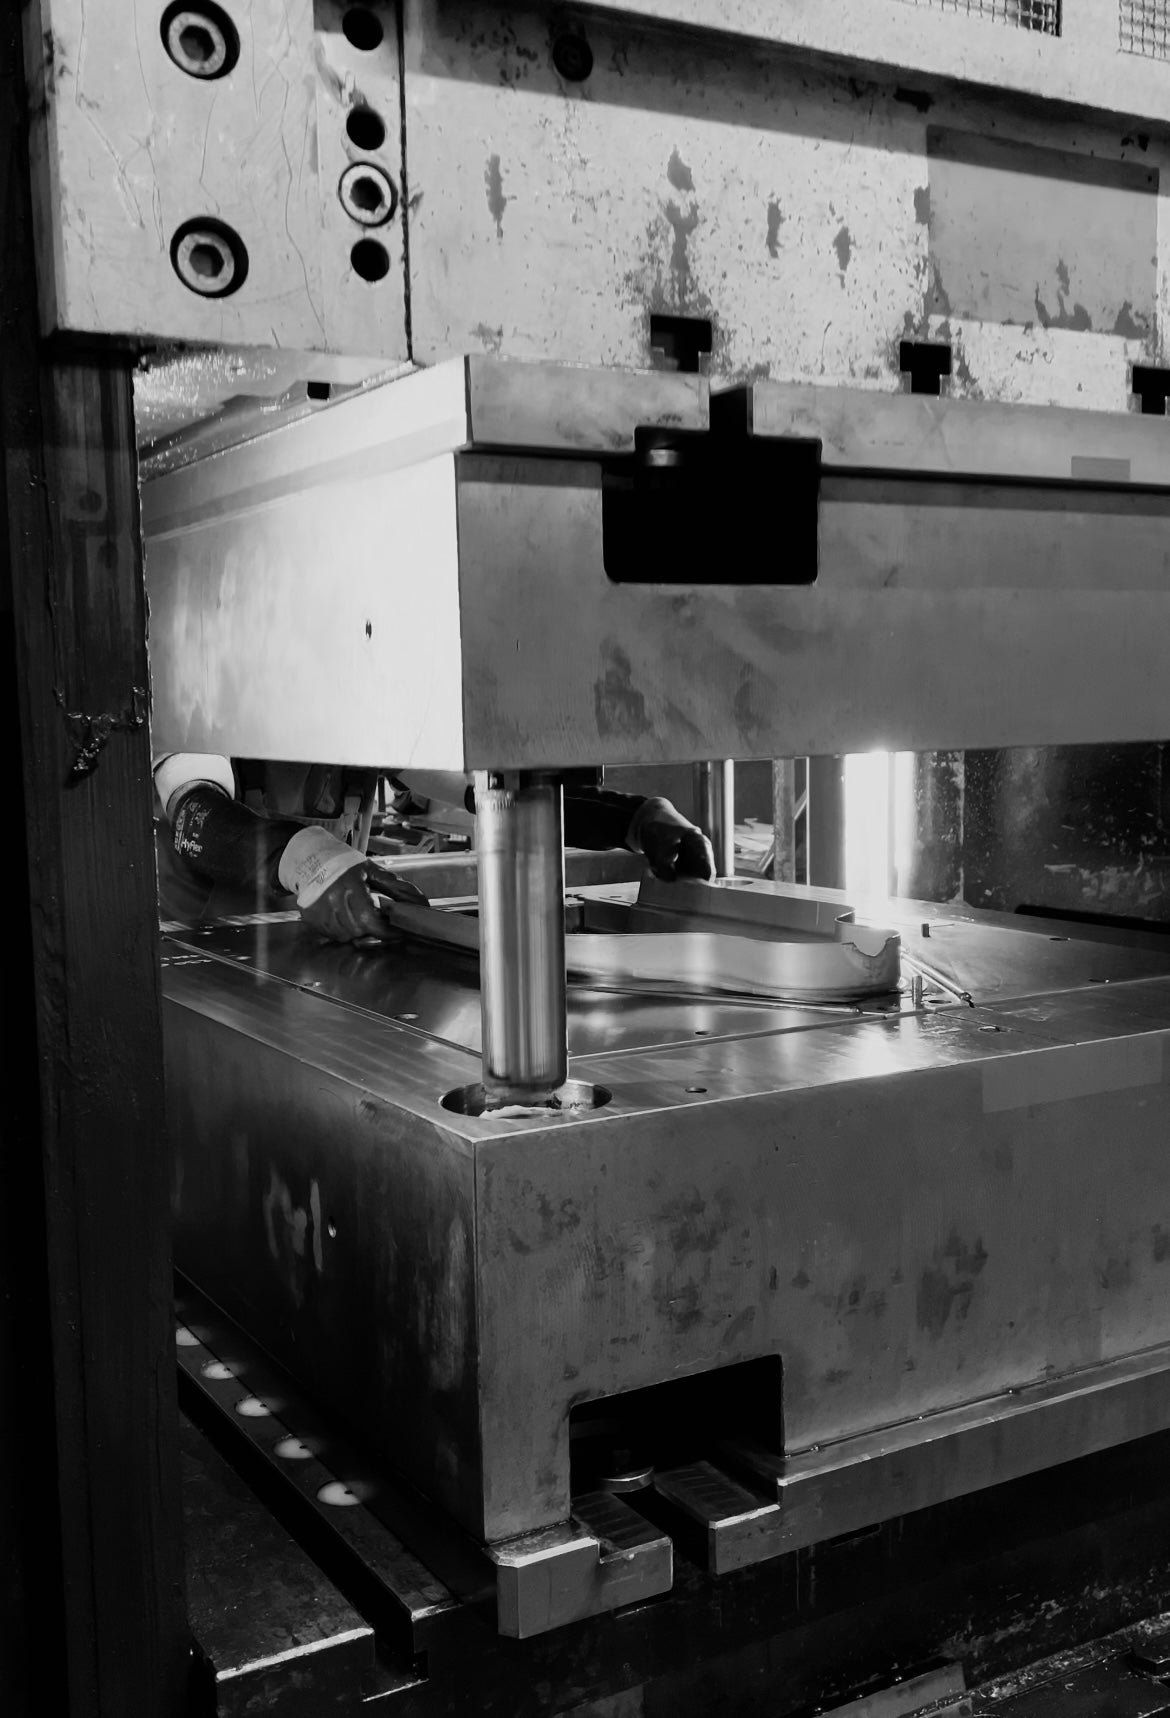
Deep drawing is our historic expertise. 53 presses of different technologies and tonnages, up to 1,000 tonnes, for technical series as well as several million parts a year.

Animated diagram
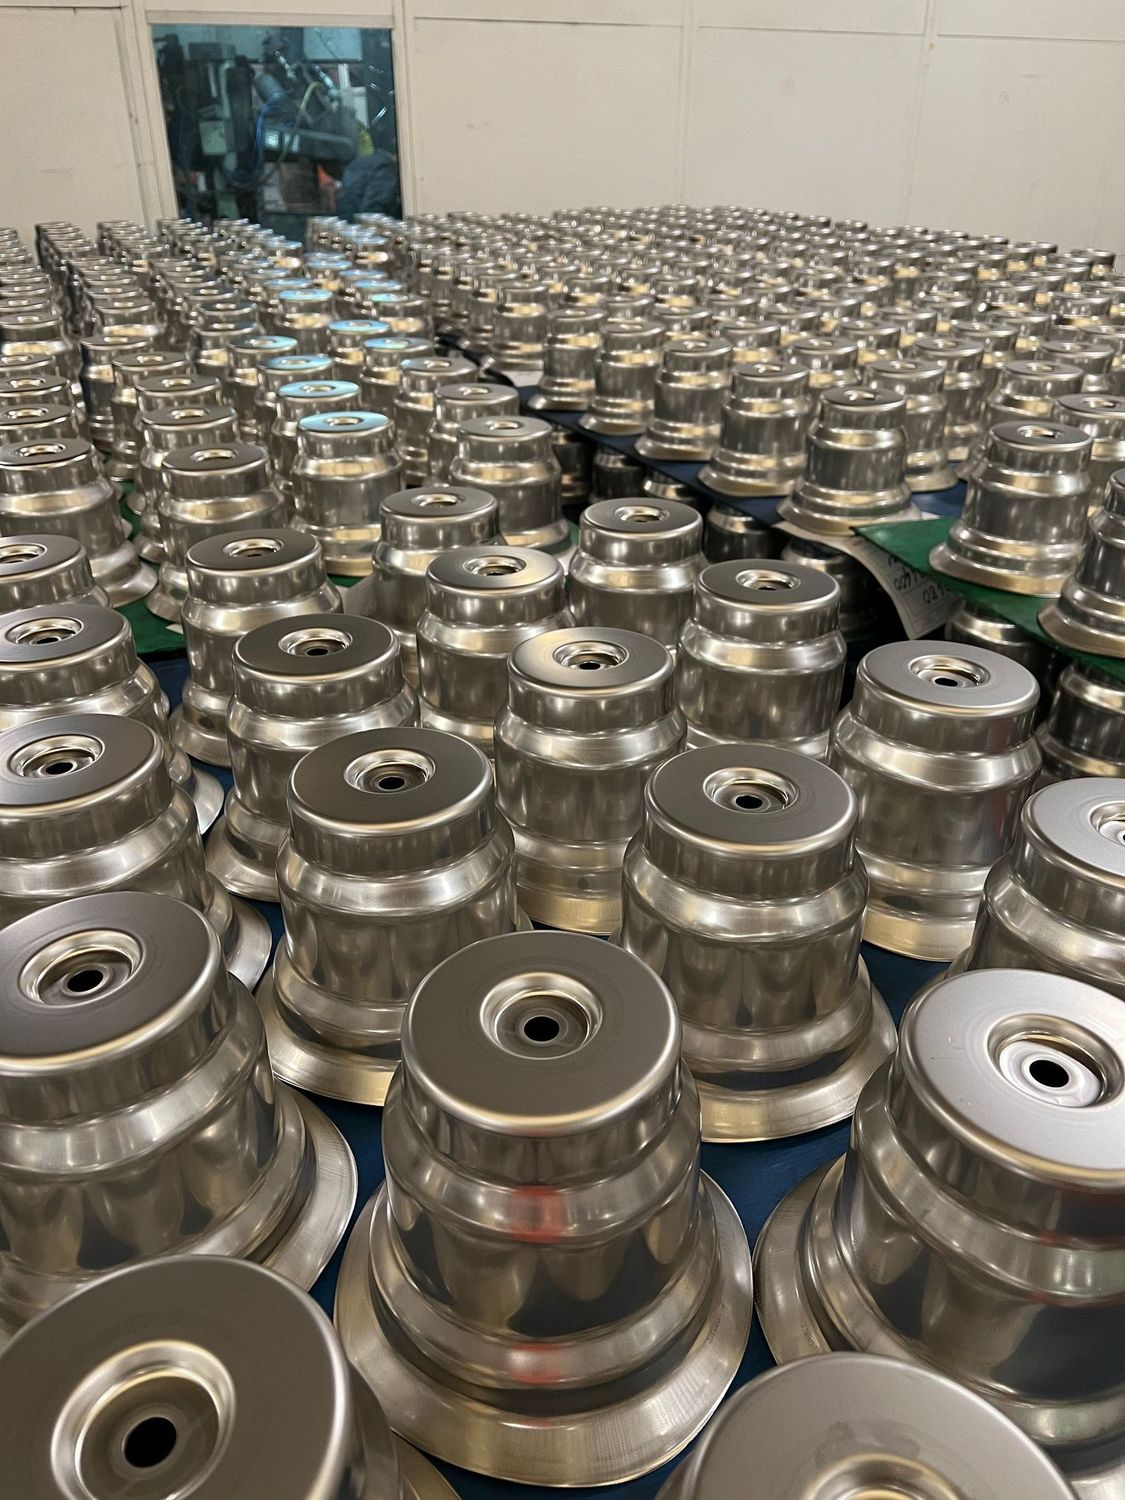
Stainless steel cups deep drawn in Vire
In the Vire workshopStainless steel cups deep drawn in Vire
Deep drawing

Cups, tanks and deep shapes

Deep, one-piece, seamless parts with high dimensional accuracy and finish. All about deep drawing →

  • IThe blank holder clamps the blank and controls draw-in
  • IIThe punch draws the metal into the die
  • IIIThe cup is ejected from the tool
  • IVFlange trimming
Presses
53, up to 1,000 t
Grades
Stainless steel 304 (18/10) and 430 (18/0)
Volumes
From prototype to several million
Precision drawing

Sizing: dimensions to the radius

The drawn cup goes back under the press in a sizing tool. The punch tightens the radii, flattens the base and compensates for springback.

  • IThe drawn cup enters the sizing tool
  • IIBefore restriking: open bottom radius, domed bottom
  • IIIThe punch tightens the radius and flattens the bottom
  • IVProfile at nominal dimension: the cup is ejected
Operation
Sizing, restrike
Result
Tighter radii and dimensions
Animated diagram
Deep-drawn and sized stainless steel parts
In the Vire workshopDeep-drawn and sized stainless steel parts
Animated diagram
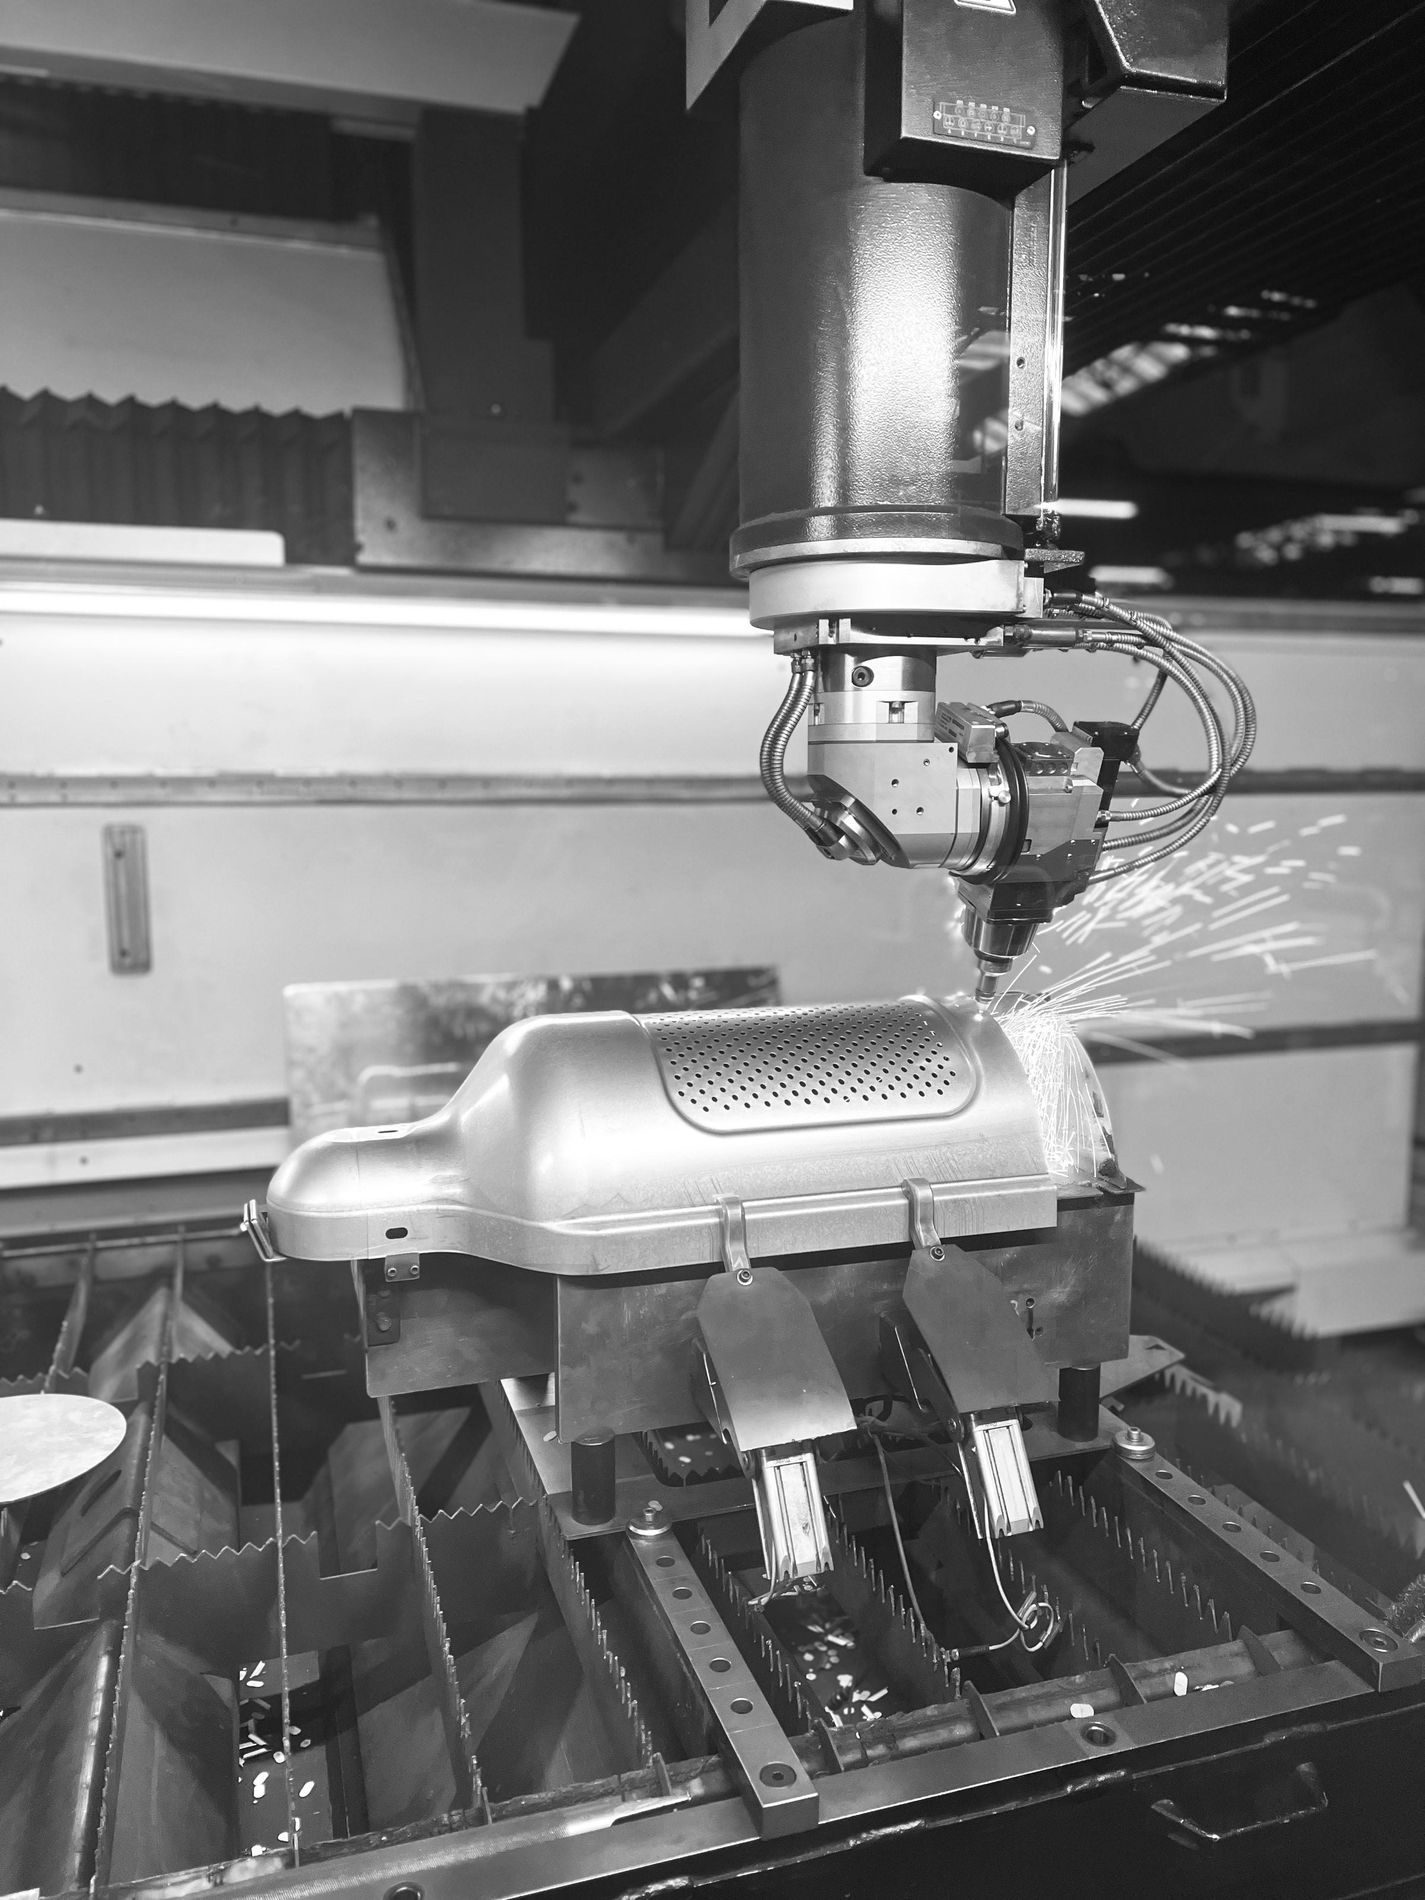
For parts that are already formed: robotic 3D laser cutting.
3D laser, in VireFor parts that are already formed: robotic 3D laser cutting.
Cutting

3D laser cutting and punching

Complex shapes laser cut on already formed parts. For large series, progressive-die punching: one press stroke, one part.

  • IProgressive tool: the strip advances one step with each press stroke
  • IIPilot holes, then the pilots centre the strip
  • IIICentre hole, then a ring of holes
  • IVTrimming: the part drops, the skeleton exits
Laser
3D cutting
Punching
Progressive die, designed in Vire
Forming
Curling, beading
Stamping

Flatware stamping and die forming

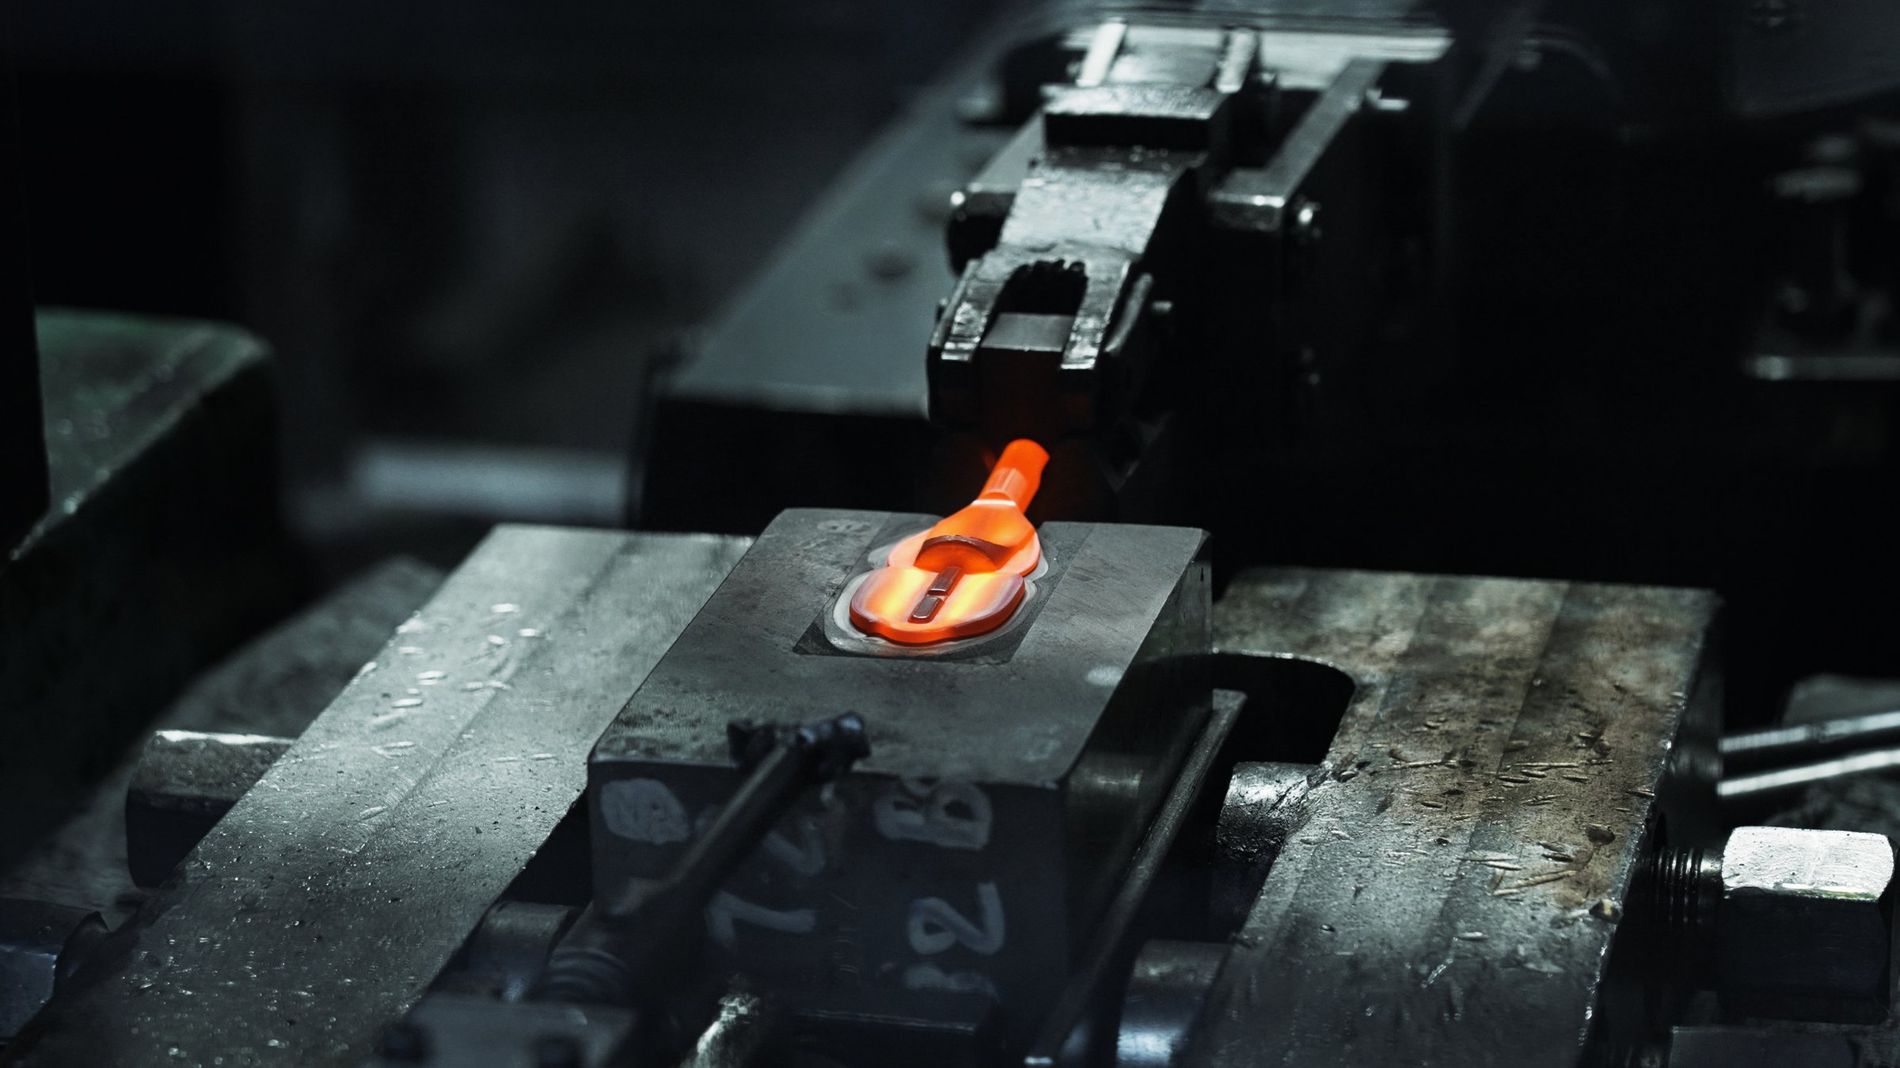
For flatware, a single press stroke on an engraved die gives both the shape and the pattern.

  • IBlank cut from the coil, then rolled
  • IITrimming: outline and tines
  • IIIStamping: shape and pattern in one stroke
  • IVEdge grinding with emery
Material
18/10 stainless steel
Tools
Dies engraved in Vire
03 · Treating and joining

Restoring the metal's ductility, then joining.

Between two drawing passes, heat treatment recrystallises the metal. Sub-assemblies are then joined by laser or TIG welding, often in robotic cells.

Animated diagram
Heat treatment

Vacuum and continuous furnaces

Work-hardened parts go into the furnace. Under vacuum, there is no oxidation: the part stays bright.

  • IWork-hardened parts loaded, furnace under vacuum
  • IIHeating without oxidation
  • IIISoak: the metal recrystallises
  • IVRapid quench under inert gas
Furnaces
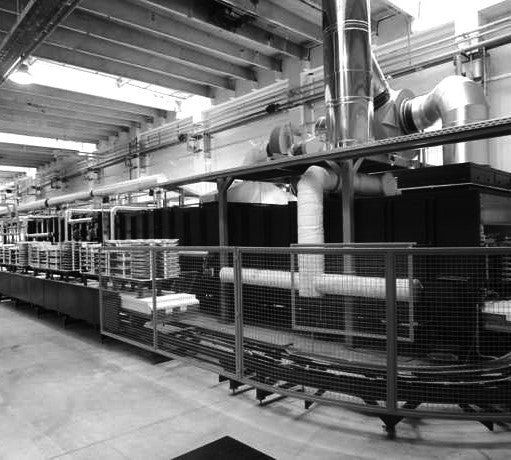
2 continuous solution-annealing furnaces
Vacuum
1 stainless steel heat-treatment furnace
Use
Annealing between passes
Welding

Laser and TIG welding

The process is chosen for each part: laser for a narrow seam with very little heat, TIG for joints that need filler metal.

  • ILaser: narrow seam, very little heat input
  • IIReduced heat-affected zone, under inert gas
  • IIITIG: tungsten electrode and filler metal
  • IVHeat tint removed during finishing
Processes
Laser, TIG
Filler
With or without filler metal
Animated diagram
Operator at an assembly station in Vire
In the Vire workshopOperator at an assembly station in Vire
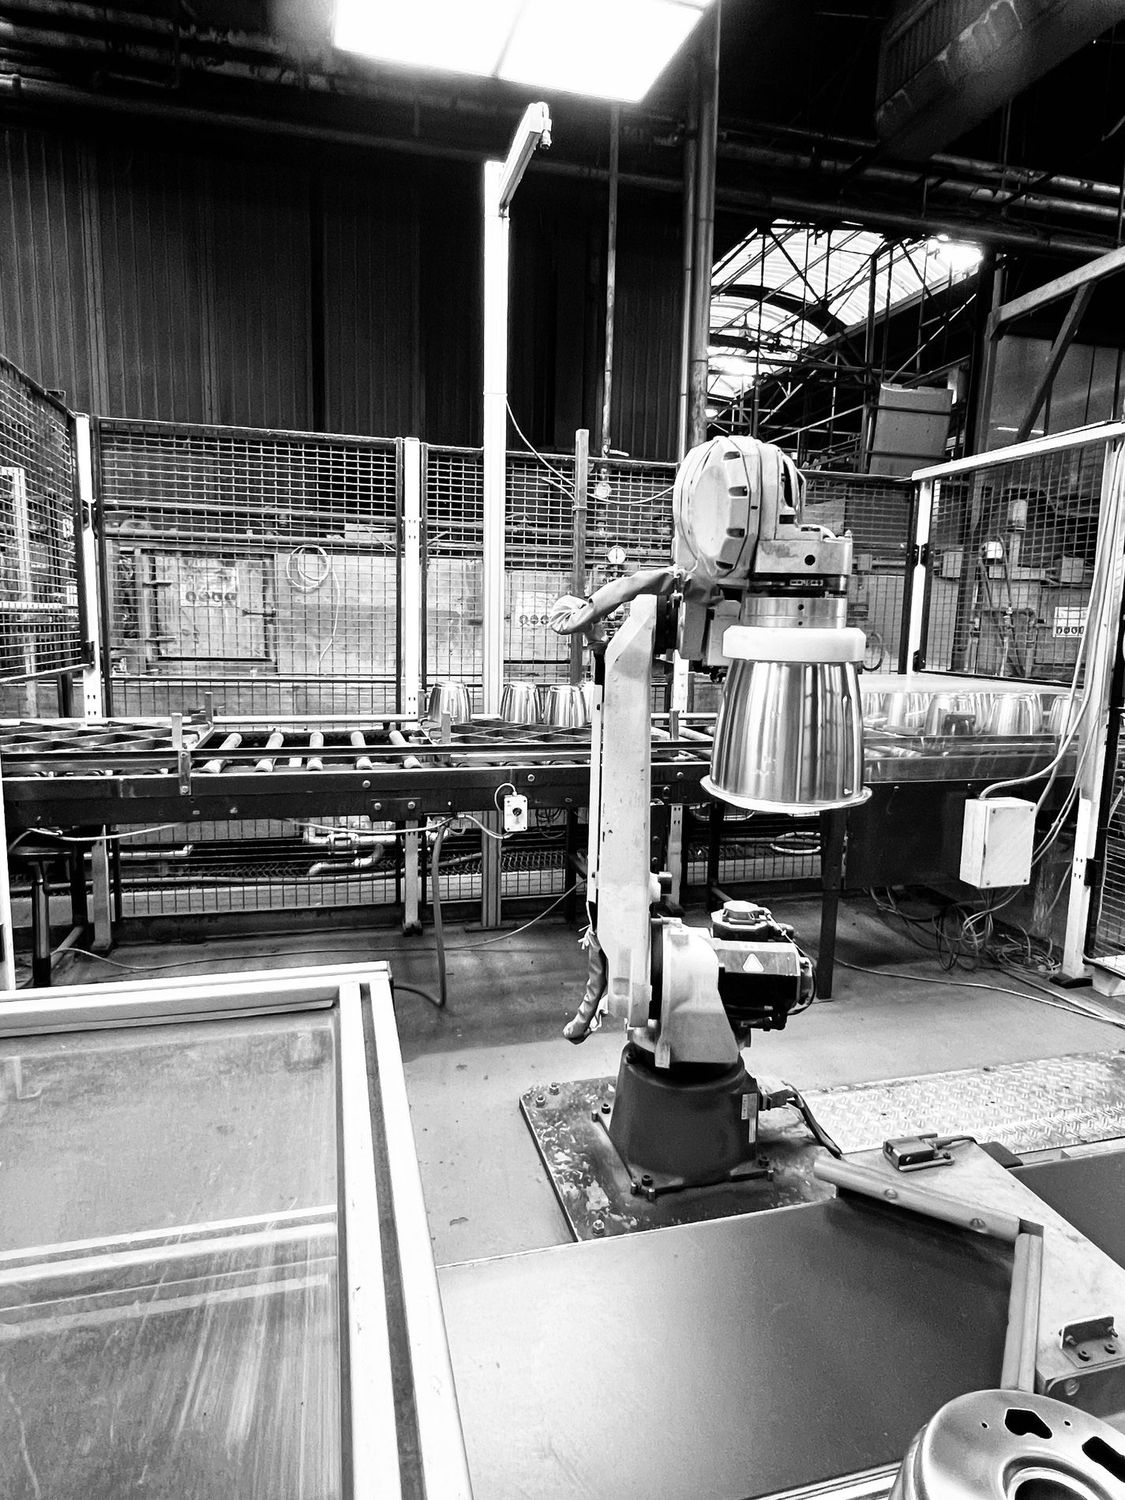
Robotic cell holding a stainless steel bowl
Robotics

28 production robots

Handling, press loading, polishing: our robotic cells deliver the output and consistency of large series.

  • IPress loading and unloading
  • IIRobotic polishing cells
  • IIIHandling between stations
Robots
28
Benefit
Output and consistency
04 · Finishing

Inside and out, all the way to mirror.

Satin, brushed, mirror polish, or both on the same part: 12 polishing carousels and robotic arms ensure a consistent finish from one part to the next.

Animated diagram
In the Vire workshopCarousel polishing on our lines.
Satin finishing and polishing

Inside and outside satin finishing, mirror polish

Every combination is possible, such as a satin interior and a mirror exterior.

  • IOutside satin finishing with abrasive belts
  • IIInside satin finishing with rotary brushes
  • IIIRobotic polishing, from satin to mirror
  • IVSatin inside, mirror outside: any combination
Carousels
12
Arms
Robotic polishing
Finishes
Satin, brushed, mirror
Blades

Blade serrating and finishing

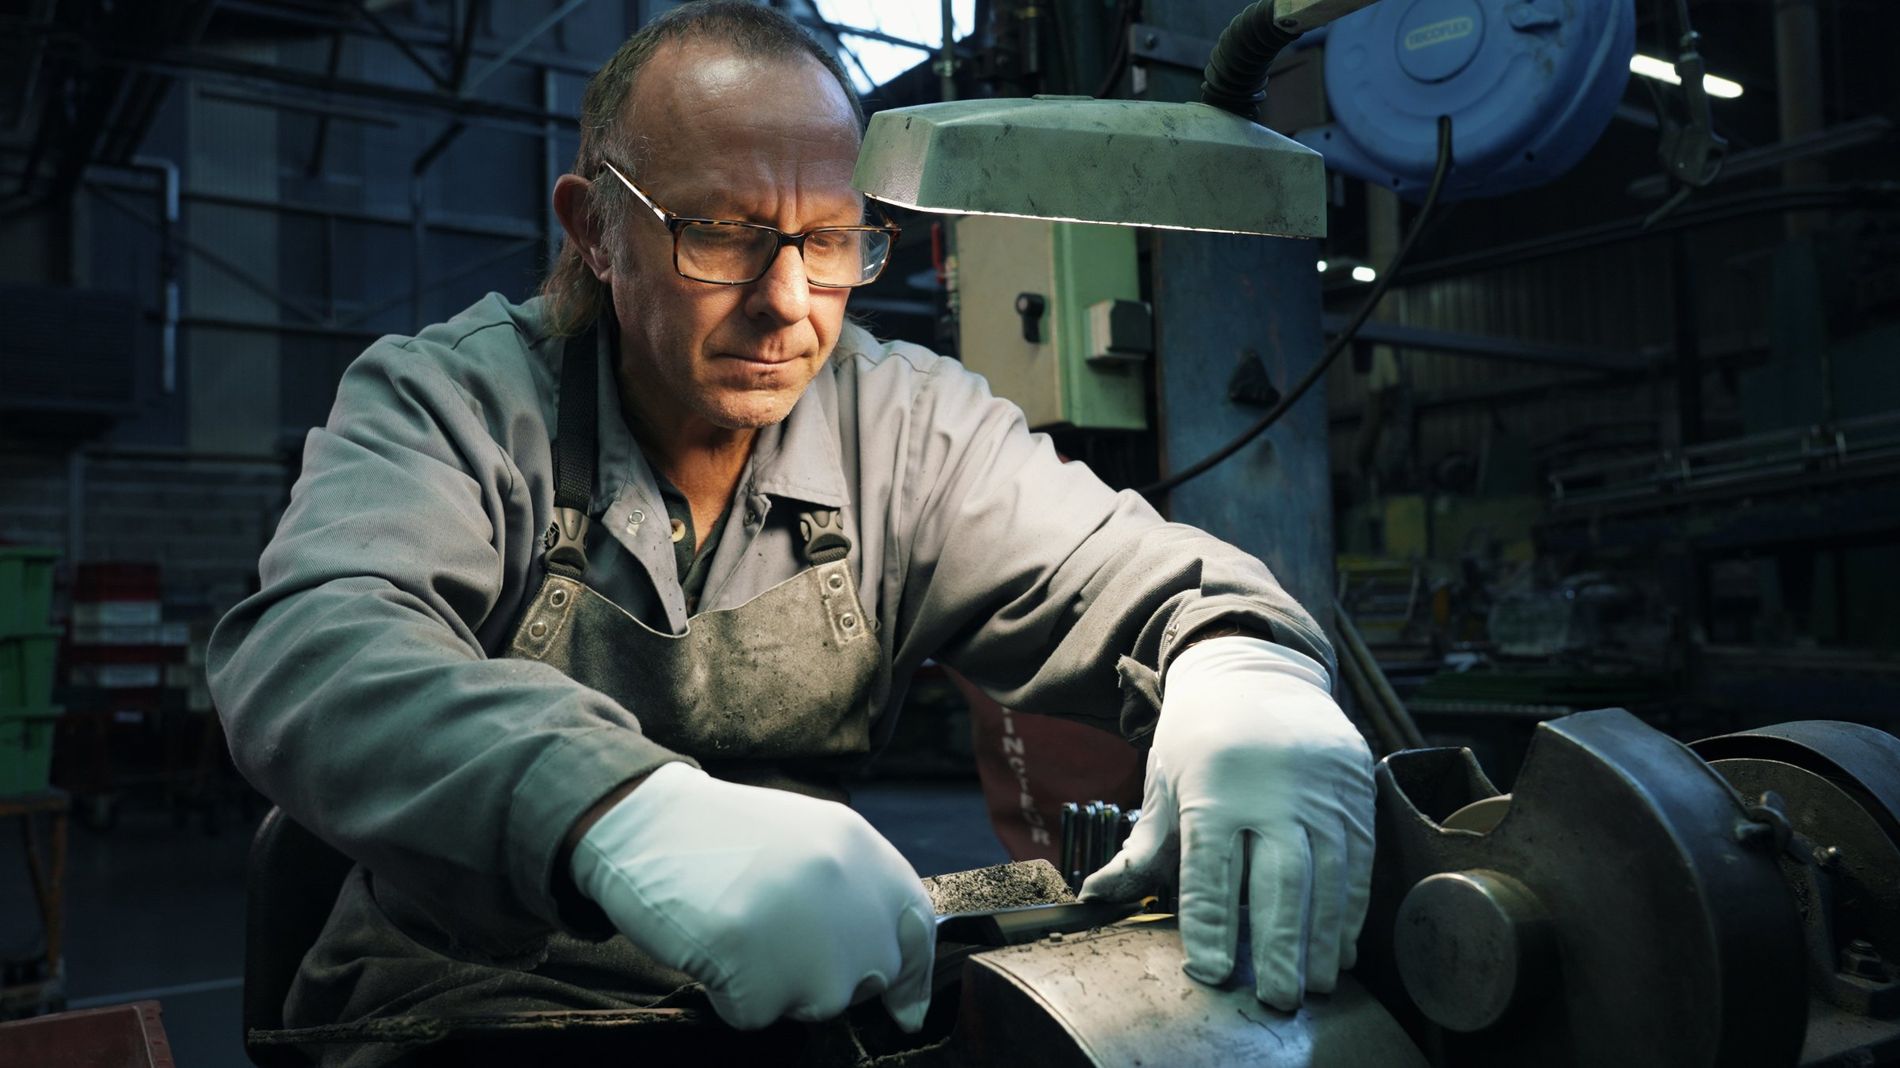
For flatware, knife blades are serrated and finished on our lines before final polishing.

  • ISerrating knife blades
  • IIEdge grinding and polishing
  • IIIVisual inspection piece by piece
Products
Table knives, steak knives
Operator serrating blades
05 · Precious metals

Gold and silver, deposited by electrolysis.

Our silversmiths silver- and gold-plate flatware, hollowware and technical parts in our electroplating workshop. Luxury clients find the plating thickness and polish quality they expect.

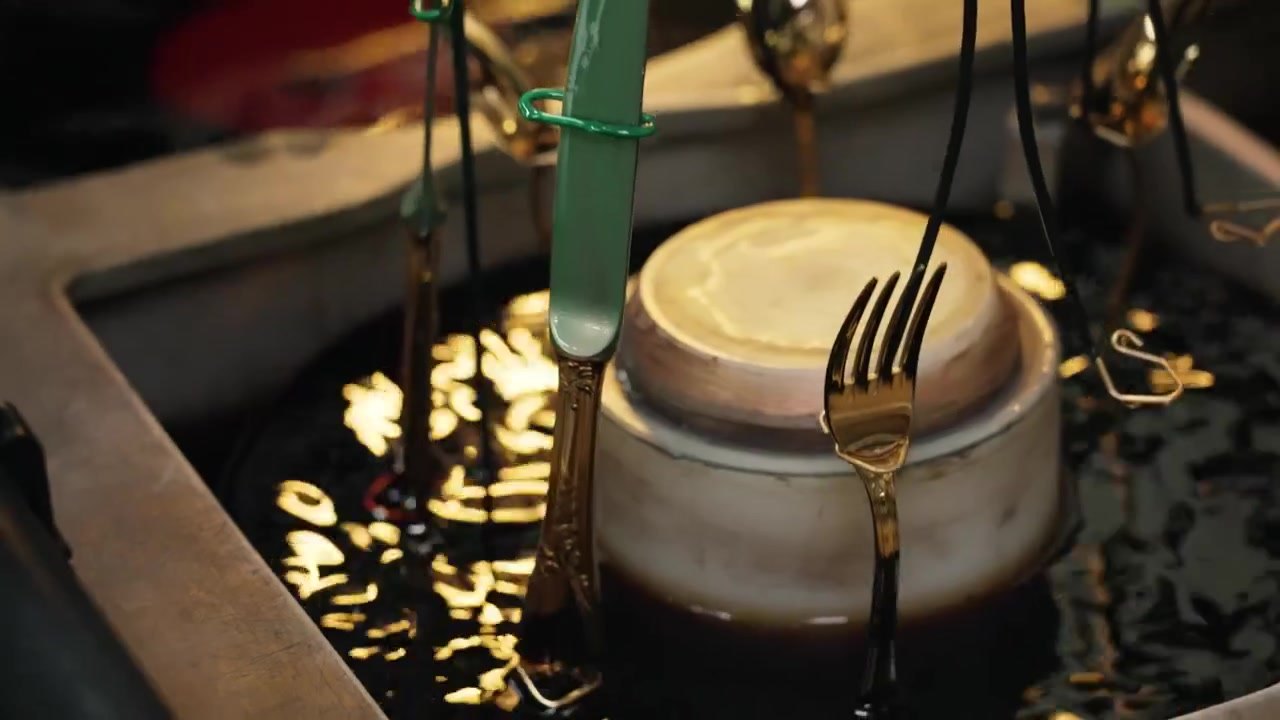
Forks in the gold plating bath Inspecting a gold-plated spoon
  • IPrepared stainless steel surface, parts mounted on the cathode bar
  • IIGold or silver deposited in the bath, under current
  • IIIThickness of your choice: 10 or 33 microns
  • IVFinal polishing by hand, on the wheel
Metals
Gold, silver
Thicknesses
10 or 33 µm
Bases
Flatware, hollowware, technical parts
Finish
Hand-polished on the wheel
Animated diagram
Flatware dipped in the gold bath, in Vire
In the Vire workshopFlatware dipped in the gold bath, in Vire
06 · Marking and customisation

Your brand, on every piece.

Die engraving, monogram stamping, laser marking, logos and bands on porcelain: customisation is done on our lines, in series.

Dies engraved with scrollwork
EngravingDies engraved with scrollwork
Monogram or pattern stamped in a single press stroke
StampingMonogram or pattern stamped in a single press stroke
Logo, text or pattern by laser
Laser markingLogo, text or pattern by laser
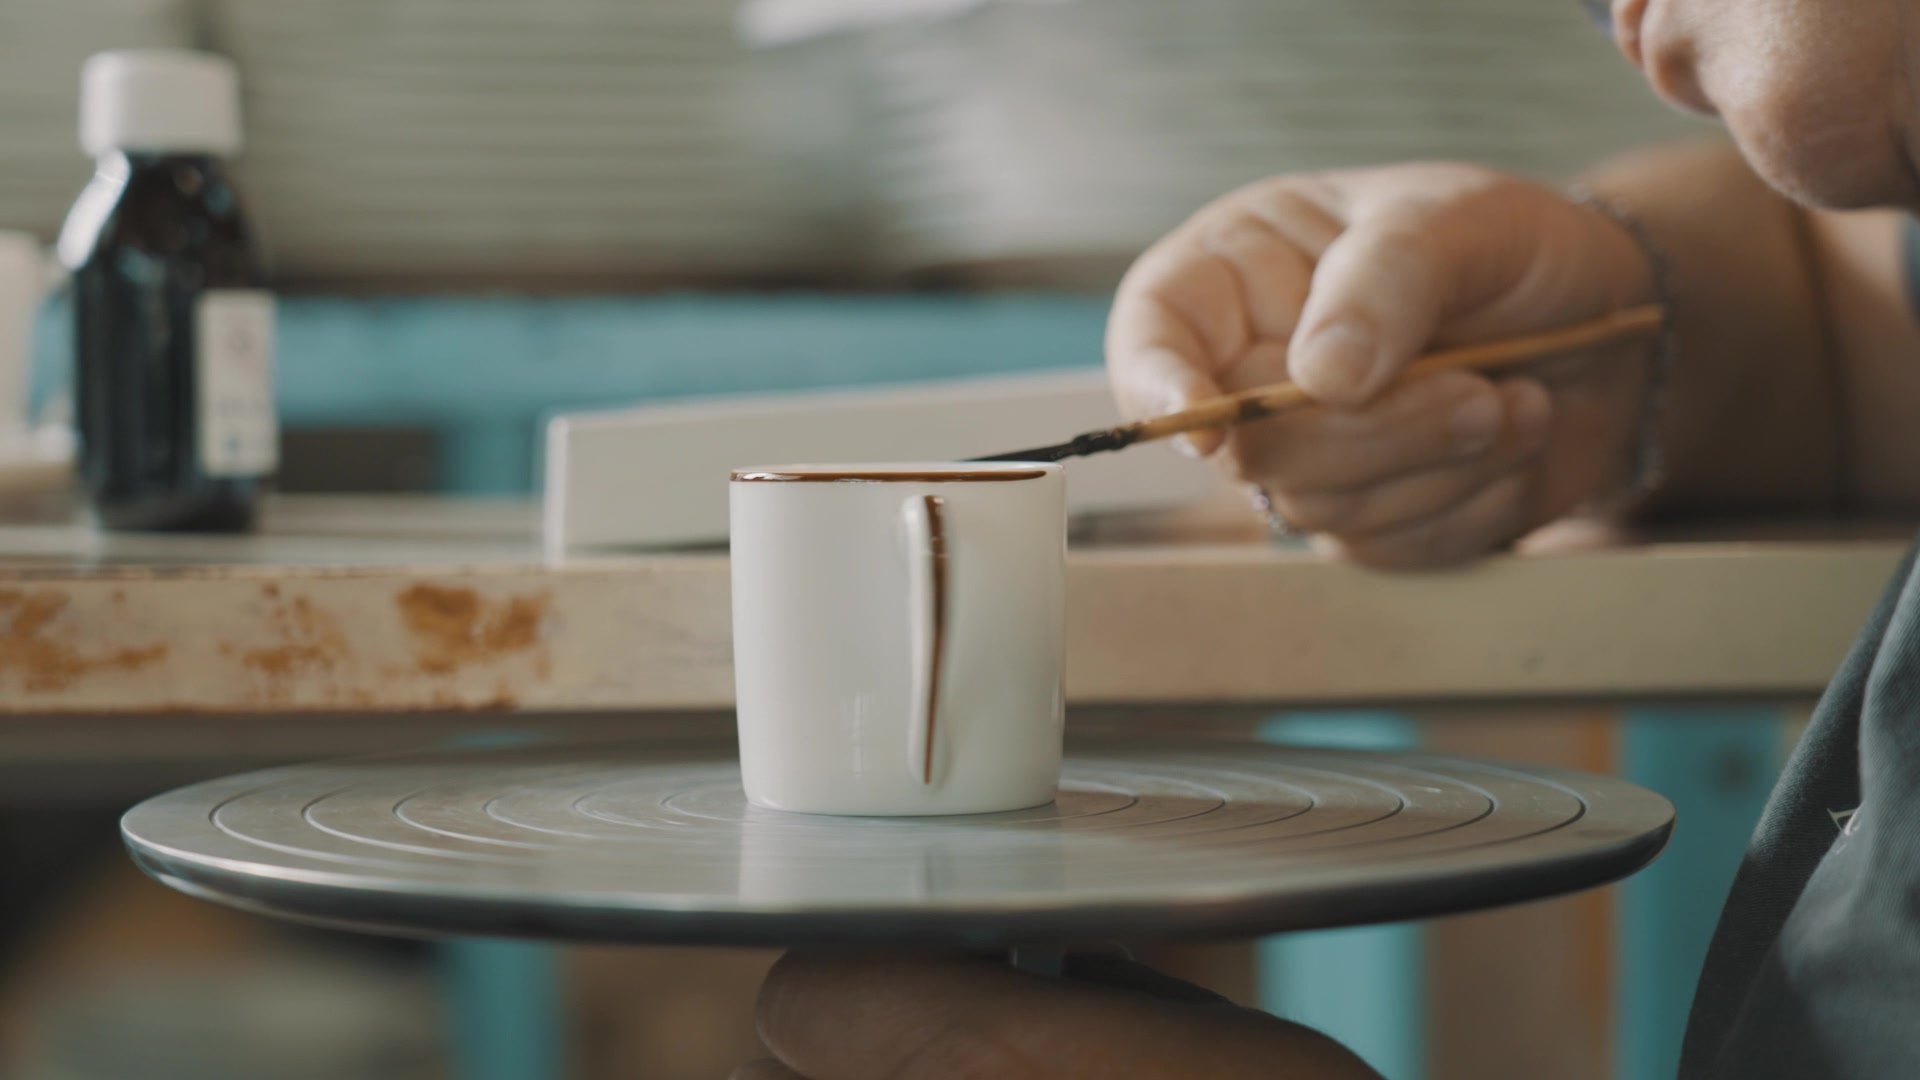
Gold band applied by hand to a cup
PorcelainGold band applied by hand to a cup
07 · Inspection

Measure before delivering.

Every batch is inspected to the tolerances of your drawing and approved in our ISO 9001 certified quality system.

Animated diagram
Two technicians checking a part in Vire
In the Vire workshopTwo technicians checking a part in Vire
Metrology

Tolerance inspection

The points defined on the client drawing are probed, then compared with the CAD model. The batch is only released once the deviation map is approved.

  • IPart placed on the surface plate
  • IIProbing of the points defined on the client drawing
  • IIIComparison with CAD: deviation map
  • IVBatch approved in our ISO 9001 system
Equipment
3D inspection area
Tolerances
Those of the client drawing
Quality
ISO 9001: 2015
08 · Porcelain

Two factories, two ways of working.

Limoges for excellence and decoration, Alföld for competitive slip casting and more complex projects in high volume.

Bisque kiln Glazing a piece

Limoges

France · 8,000 m²
  • Isostatic pressing and jiggering
  • Slip casting
  • Bisque firing at 960 °C, glazing, decoration firing
  • Decoration: decals, hand-painted bands, logos
  • Backstamping and piece-by-piece finishing
Capacity
≈ 1 million pieces / year
Designation
Limoges porcelain, PGI
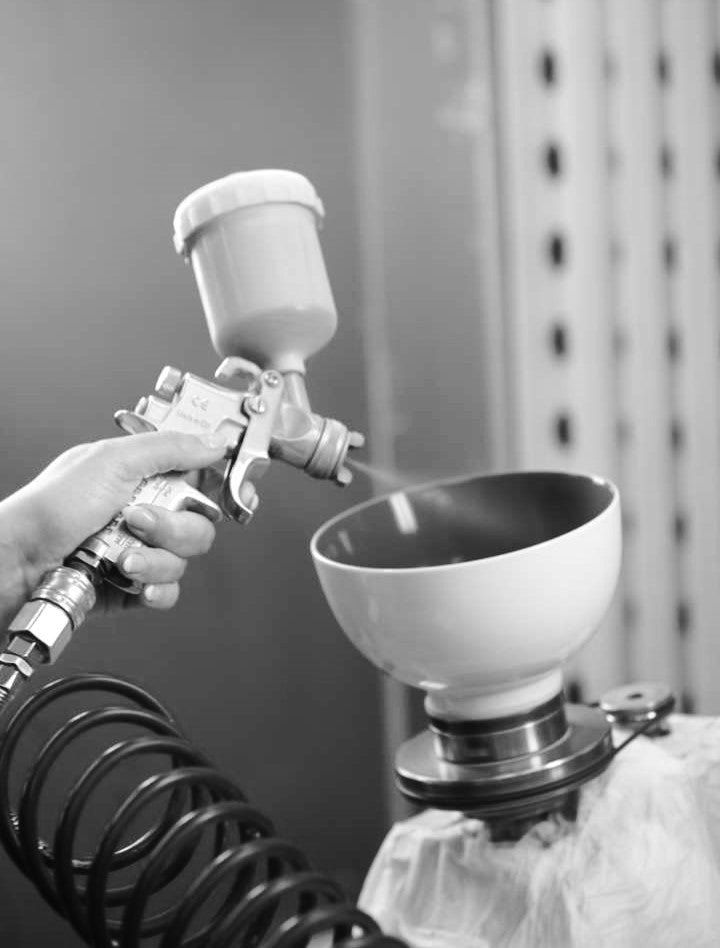
Kiln at the Alföld factory Spray colouring Porcelain inspection Production line at the Alföld factory

Alföld

Hungary · 40,000 m²
  • Competitive slip casting, including complex shapes
  • White body and coloured body
  • Spray colouring
  • Brush decoration
  • Tailor-made solutions for industry
Capacity
≈ 1,000 t, i.e. ≈ 3.2 M pieces / year
Quality
ISO 9001
Machinery · Vire

Everything under one roof.

Industry brochure (PDF)
Equipment Number Use
Presses53Drawing, cutting, stamping · up to 1,000 t
Robots28Handling, press loading, polishing
Polishing carousels12Satin finishing, polishing, mirror polish
Continuous solution-annealing furnaces2Continuous heat treatment
Vacuum heat-treatment furnace1Oxidation-free annealing
3D laser cutting—Cutting of formed parts
Blanking lines5Blank cutting
Laser and TIG welding—Sub-assembly joining
Spot welders8Spot-welded assembly
BrazingHF · inductionHigh-frequency and induction brazing
Manual polishing wheels20Polishing and finishing by hand
Vibratory finishers5Deburring and mass finishing
Metal 3D printing (SLM)—Steel prototypes
Machining resources—Tool making
3D inspection area—Metrology, comparison with CAD
Electroplating bathsGold · Silver10 or 33 µm deposits

Our presses include 15 hydraulic presses from 150 to 600 t, 20 mechanical presses, 4 mechanical transfer presses from 32 to 630 t and a CNC line of 4 hydraulic transfer presses.

FAQ

Frequently asked questions.

Which technologies are performed in-house?

Engineering office and simulation, metal 3D prototyping, tooling, deep and precision drawing, 3D laser cutting, punching, curling, heat treatment, laser and TIG welding, satin finishing, polishing, silver plating, gold plating, engraving, laser marking and inspection. For porcelain: isostatic pressing, jiggering, slip casting, glazing and decoration.

What is the capacity of your presses?

Our fleet includes 53 presses of different technologies and tonnages, up to 1,000 tonnes for the most powerful.

Do you make prototypes?

Yes. Our steel prototypes are 3D printed by laser powder bed fusion, to validate shape and handling before tooling is launched.

What are your certifications?

Our quality system is ISO 9001:2015 certified by Apave Certification, a body accredited by Cofrac, the French accreditation committee (certificate no. 698479, valid until August 2027). Our CSR approach earned an EcoVadis silver medal, and the house holds the Entreprise du Patrimoine Vivant label.

Go further

Guides from our engineering office.

All guides

A drawing, an idea, a series to bring back?

Talk about your project Flatware subcontracting
Request a quote